

『Advantages and Disadvantages of Vortex Flow Meter: Steam Monitor Pro/Con Sizing』Related information(clamp on meter|electromagnetic meter|venturi meterrotameter|orifice meter|ultrasonic flow meter|mass flow meter|coriolis mass flow meter|coriolis flow meter|magnetic flow meter|magmeter flow meter|magflow flow meter|mag meter flow meter|electromagnetic flow meter|vortex flow meter|turbine flow meter|thermal mass flow meter|thermal flow meter|rotameter flow meter)
Advantages and Disadvantages of Vortex Flow Meter: Steam Monitor Pro/Con Sizing
Quick Answer: For steam pipes from DN25 to DN200, a vortex flow meter gives direct volume flow and can output mass flow with pressure or temperature compensation. The main advantages are no moving parts, wide range, and lower long term cost. The main limits are low flow cutoff, vibration sensitivity, and straight run needs.
How a Vortex Flow Meter Works in Steam Service
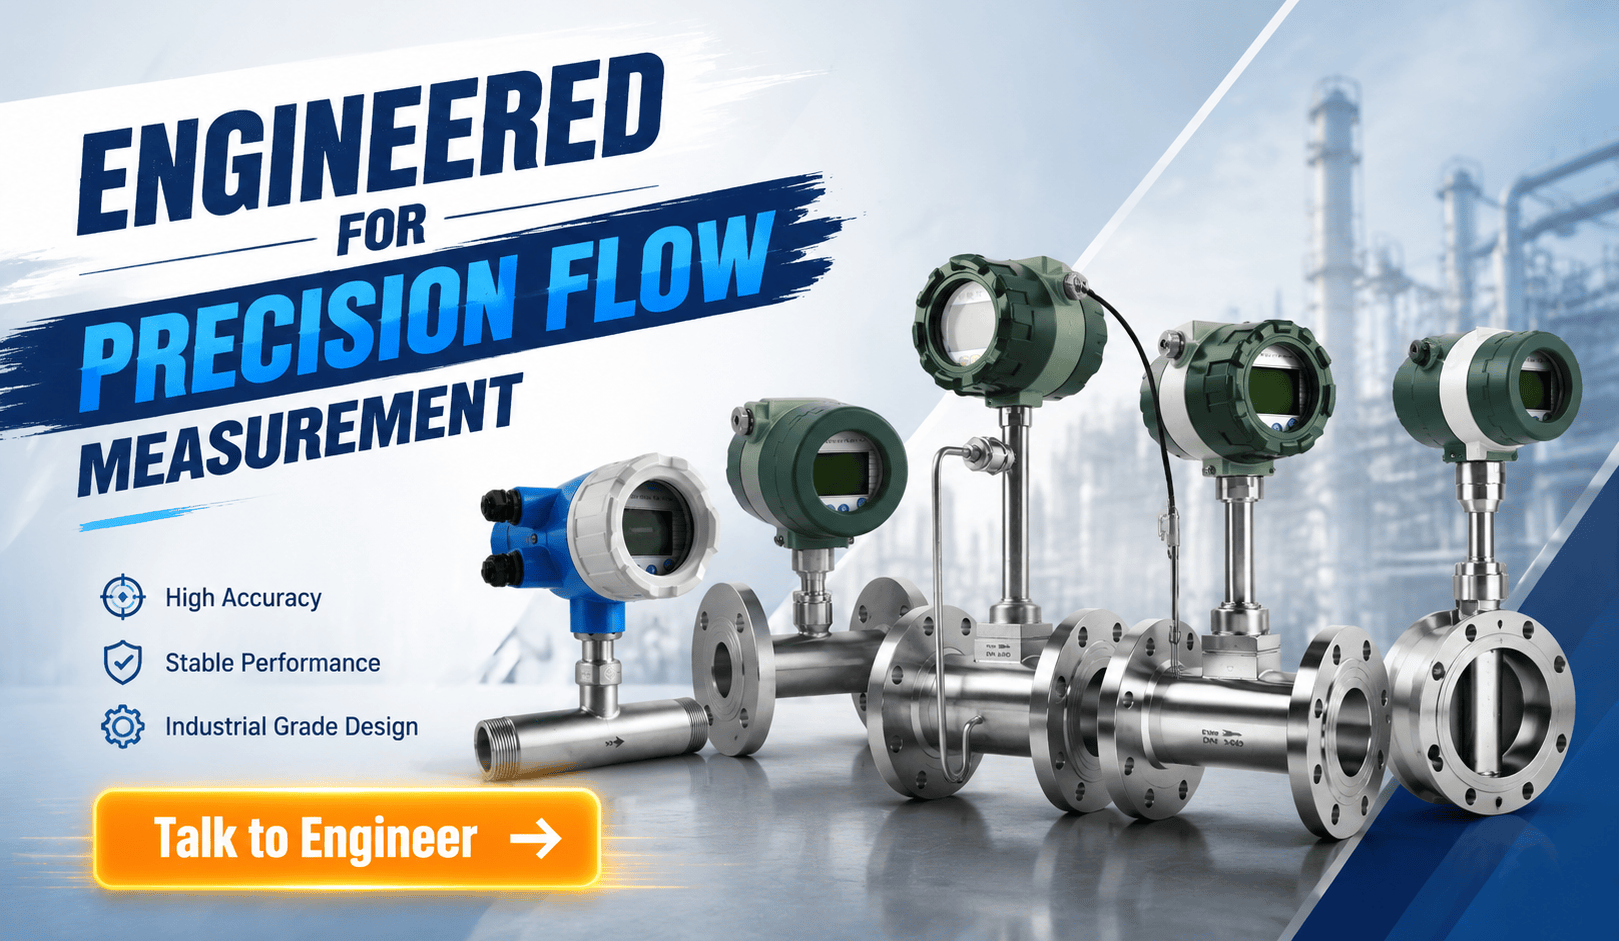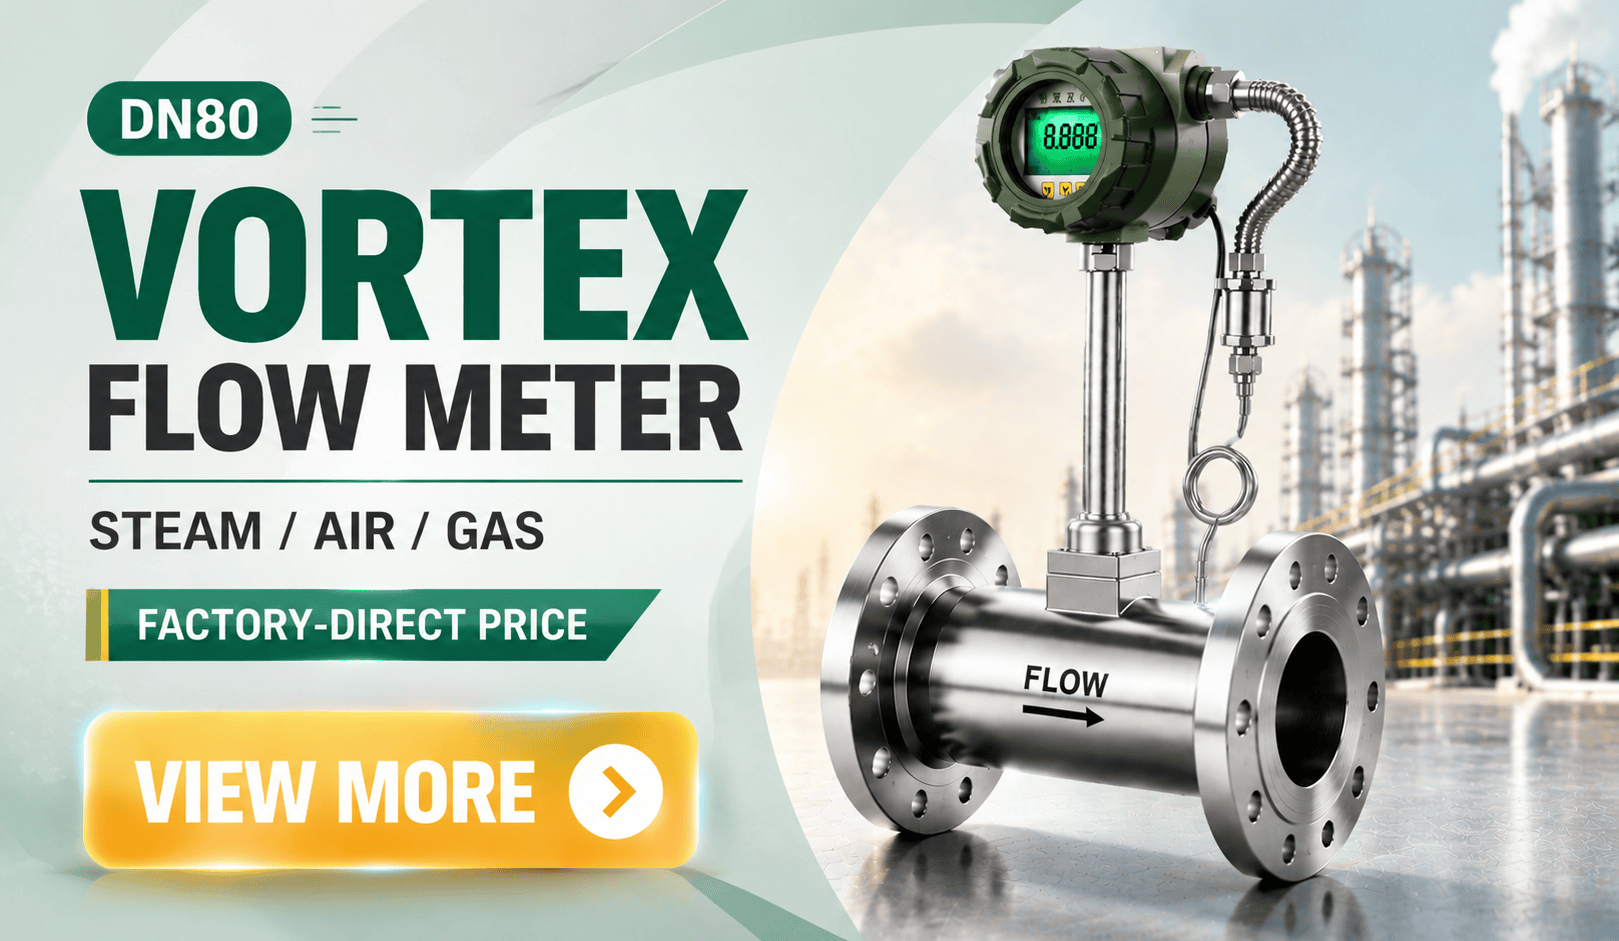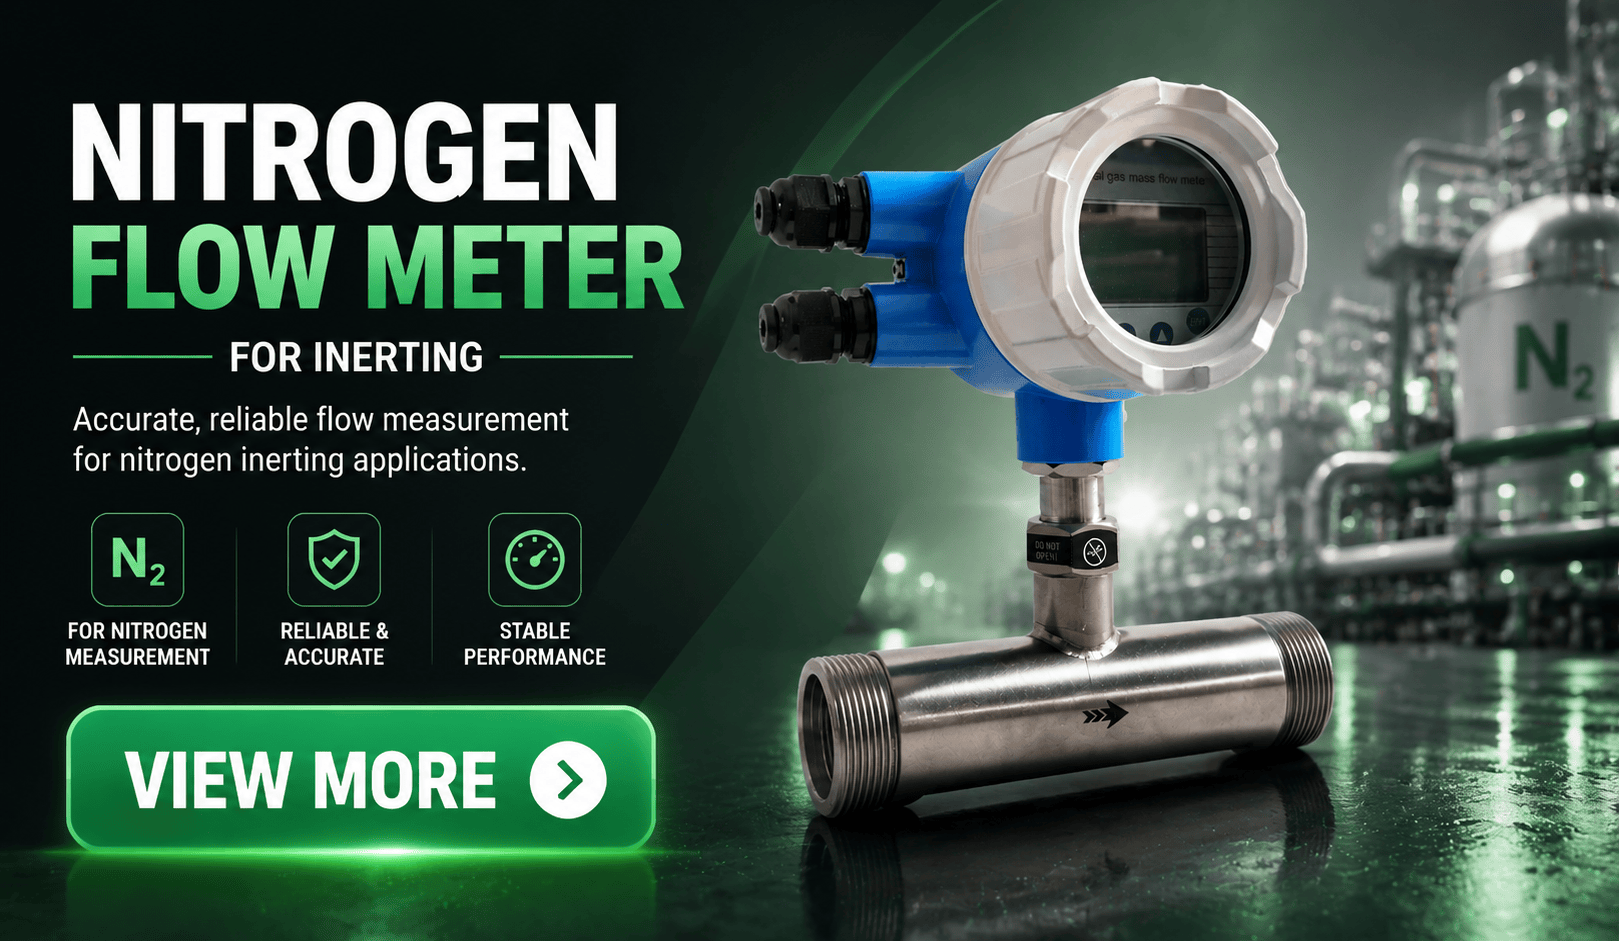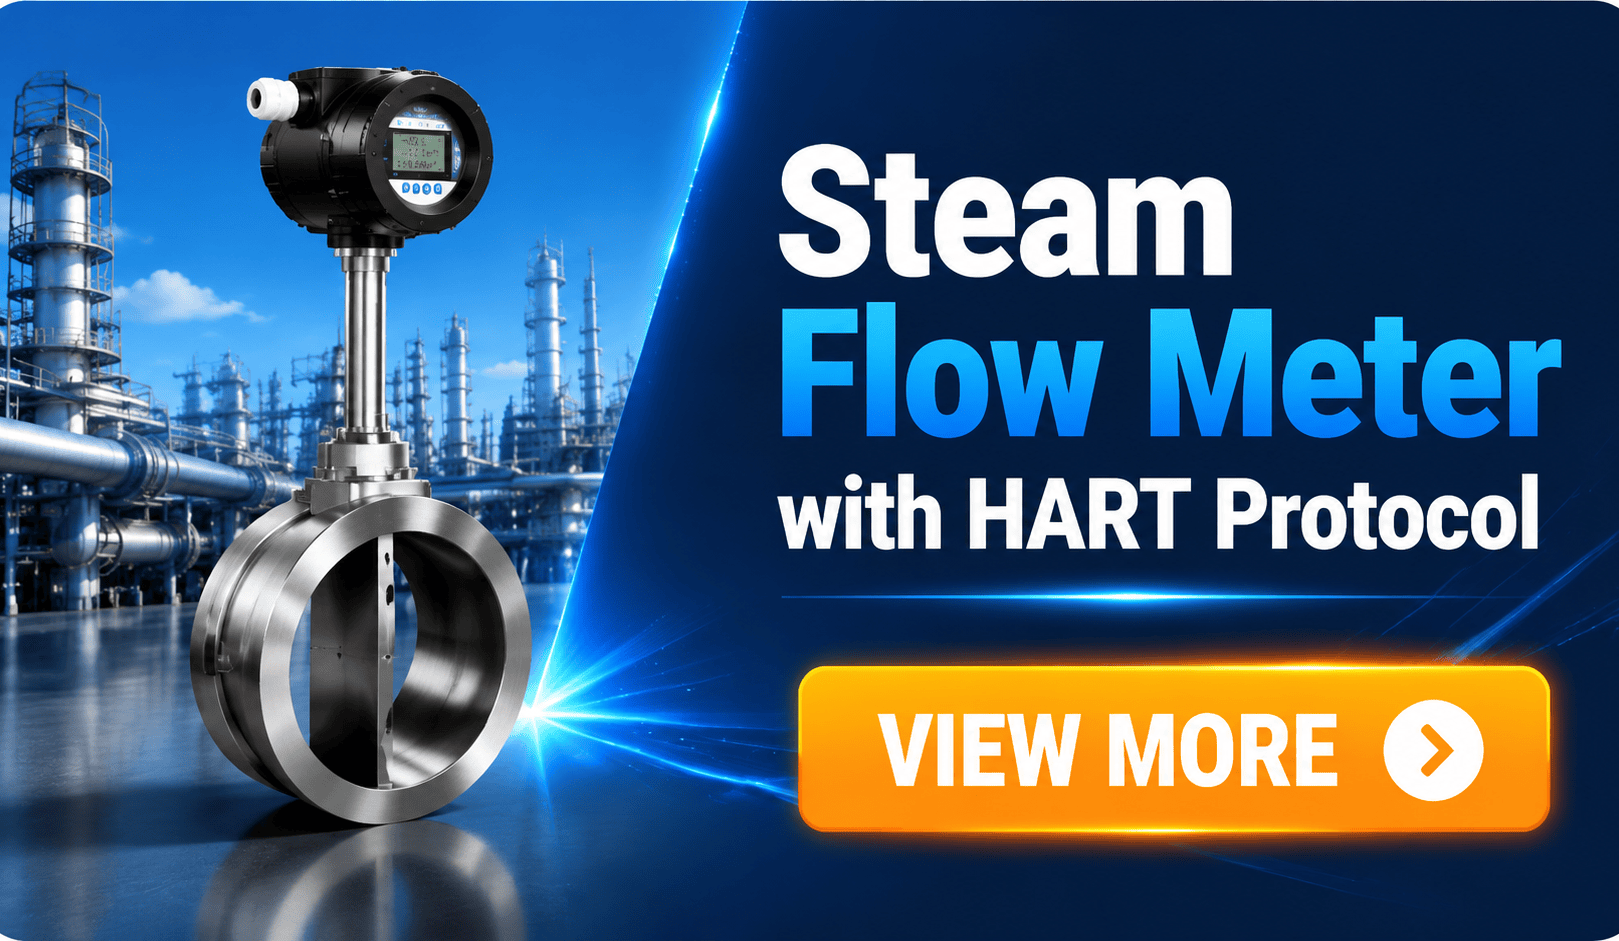
In a steam line, the meter uses a bluff body to create vortices. A sensor detects vortex frequency and converts it into flow velocity. Because steam density changes with pressure and temperature, a standard vortex meter reads actual volume flow. For mass flow in kg/h, use a multivariable transmitter with an integrated PT100 and pressure input. Silver Automation Instruments supplies DN15 to DN300 vortex steam meters with 4-20 mA HART output.
Main Advantages for Steam Monitoring
No moving parts is the first advantage. A sensor sits outside the flow path or behind a protective diaphragm. In a palm oil mill in Malaysia, a DN100 vortex meter on a 12 bar saturated steam header ran for four years with no maintenance and no drift beyond 1 percent. Steam plants want that kind of reliability.
Wide turndown is the second advantage. For steam at 10 bar and 180°C, a DN50 vortex meter can measure from about 80 kg/h to 2400 kg/h when line velocity stays between 7 m/s and 45 m/s. That range covers most batch boilers and process loads. Most engineers skip this part and size by pipe diameter only. Sizing by pipe diameter only creates poor accuracy at low load.
Direct volume output is the third plus. A vortex meter produces a frequency signal linear to flow. There are no DP taps, no impulse lines, and no condensate pots. A food plant in the Philippines replaced a DP flow element with a DN65 vortex meter because impulse lines clogged with boiler scale. The meter now sends 4-20 mA HART to the boiler control panel.
Pressure loss is low. A vortex meter adds a small permanent pressure loss, typically around 2 percent of line pressure at maximum flow. For a plant running at 8 bar, the loss is lower than most orifice plate installations. Lower pressure loss can mean less fuel gas fired in the boiler.
Main Disadvantages and Sizing Limits
Vortex meters do not measure very low flow. At Reynolds numbers below 10000 to 20000, vortex shedding becomes unstable. The meter cuts off around 5 to 8 percent of maximum flow depending on pipe size and steam density. If your steam demand swings from full load to almost zero at night, a vortex meter may miss that small flow. Some engineers add a second meter or accept the cutoff.
The meter is also sensitive to vibration. Piston compressors, boiler feed pumps, and steam traps can create pipe vibration. If vibration exceeds 1 g, the sensor may read false flow. Use a flow straightener, move the meter away from the pump, or choose a dual sensor design with vibration filtering. A mining site in Western Australia had false readings on a DN40 vortex meter installed near a reciprocating pump. Moving the meter 10 pipe diameters downstream solved the problem.
Straight pipe requirements are real. For a standard vortex steam meter, plan for 15D upstream and 5D downstream when one elbow or tee is present. If a control valve sits upstream, use 30D or a flow conditioner. A short straight run changes accuracy by 1 to 3 percent, often enough to fail an energy audit.
Temperature range is another point. Standard vortex meters often cover up to 250°C. For superheated steam above 250°C, specify a high temperature version with a remote transmitter or an extended sensor. Silver Automation Instruments offers high temperature versions up to 350°C.
Steam Sizing That Most Engineers Skip
In practice, sizing is where most vortex meter problems start. Here is the thing. Do not size a vortex meter by pipe diameter alone. Calculate steam velocity at minimum and maximum load. For saturated steam, aim for 20 to 35 m/s at normal load. For superheated steam, you can go up to 50 m/s but keep sensor temperature and pressure rating in check.
Here is a real case. A customer in Vietnam asked for a DN80 vortex flow meter for a 6 bar saturated steam line. The line size was DN80, but normal load was only 150 kg/h. At 6 bar, saturated steam density is about 3.6 kg/m3. At 150 k
For saturated steam, temperature and pressure are linked. You can use a temperature input or a pressure input for density compensation. For superheated steam, you need both pressure and temperature. A multivariable vortex meter from Silver Automation Instruments accepts a PT100 signal and a pressure transmitter signal. The meter outputs mass flow in kg/h directly. The multivariable setup works well for steam boiler monitoring and distribution headers.
Pipe size and flange standard matter too. A DN50 vortex meter with wafer body is lighter and cheaper for PN16 lines. A DN80 flange style meter fits ANSI 150 or DIN PN40 systems. Always state the flange standard when you request a quote. Otherwise you can receive a meter that does not match your existing bolt pattern.
Where Vortex Steam Meters Work Best
We have supplied vortex steam meters to palm oil mills in Malaysia, textile plants in Bangladesh, dairy processing in New Zealand, and chemical batch reactors in the Middle East. Most customers use 4-20 mA HART output. Some add RS485 Modbus for energy monitoring. A dairy plant in Queensland uses a DN50 vortex meter on a 9 bar steam line. The meter paid for itself in six months because the plant found a steam trap leak losing 80 kg/h.
At flow-meter.com.au, we stock stainless steel body vortex meters for steam and gas. The wafer style covers DN15 to DN300. Flange style options match ANSI 150 or 300 class and DIN PN16 or PN40. Standard process temperature is up to 250°C and high temperature versions go to 350°C. ATEX Zone 1 approved electronics are available. We also supply PT100 sensors and pressure transmitters for mass flow compensation.
Cost and Maintenance Comparison
Compared to an orifice plate, a vortex meter usually costs more at purchase but less to operate. An orifice plate needs a DP transmitter, a manifold, impulse tubing, and regular leak checks. A vortex meter is one device with one transmitter. Over five years, the vortex meter is cheaper because there are no impulse lines to rod out and no DP transmitter drift. For steam lines below DN25, a vortex meter may not fit well. In that case, steam load is often too low for a vortex meter anyway. A correct sizing review is needed before you buy.
Frequently Asked Questions
Can a vortex flow meter measure low pressure steam below 2 bar?
Yes but sizing is harder. Low pressure steam has low density, so velocity is high for the same mass flow. Minimum mass flow may still fall below the meter cutoff. Use a smaller meter or raise upstream pressure. Send us the actual pressure and load and we will check the sizing.
What is the accuracy of a vortex steam meter?
For steam, typical accuracy is ±1.5 percent of reading above minimum velocity. Repeatability is around ±0.25 percent. With density compensation, mass flow accuracy is often ±2 percent of reading depending on PT100 and pressure transmitter errors.
How long does straight pipe need to be?
Plan on 15D upstream and 5D downstream as a minimum. With a control valve upstream, use 30D or install a flow conditioner. Avoid two elbows in different planes directly upstream.
Can I use a vortex meter for superheated steam?
Yes. Specify a high temperature version for steam above 250°C. For superheated steam, use both pressure and temperature compensation because density depends on two variables.
What does Silver Automation Instruments need for a steam meter quote?
Send us your pressure in bar, temperature in °C, pipe size in DN, and minimum and maximum flow range in kg/h. Also tell us the flange standard and whether you need ATEX Zone 1 approval. We will return a sizing sheet and a price.
As a flow meter manufacturer and supplier, Silver Automation Instruments handles steam meter sizing in house. Send us your pressure (bar), temperature (°C), pipe size (DN), and flow range (kg/h). Our engineers will select the correct meter size and send a quote. Tel: +86-135-1213-1526, Whatsapp: 86-135-12131526, WeChat: +86 13512131526. You can also visit flow-meter.com.au. Please send the four values and we will return a sizing sheet.
 Hot News
 Related AD